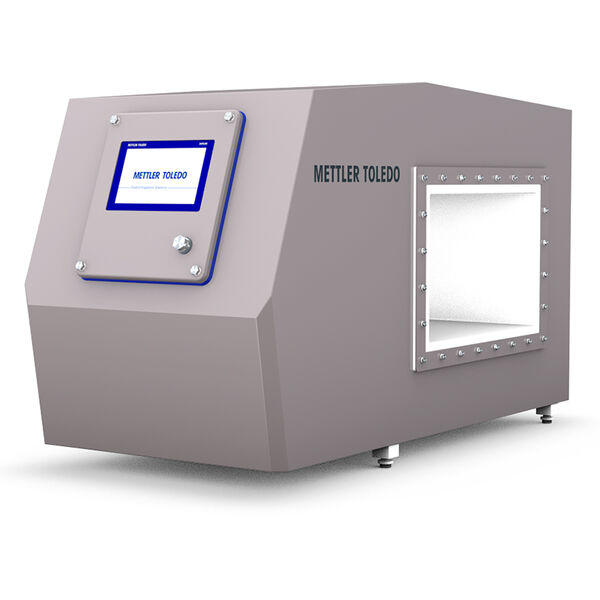
Metal detectors for bulk product inspection play a critical role in checking for metal contamination in bulk products, such as sacks of powders, grains or granules, and large crates or blocks of deep-frozen meat or produce. The large volume of dry, bulk, packaged products such as 50-kilogram sacks of flour, sugar and coffee can make inspection more difficult. These types of applications require specialized metal detection technology to address a challenge called "bulk effect". Bulk effect occurs when the greater quantity of material being inspected impacts the metal detector’s sensitivity.
To address this challenge, advanced metal detectors use high-tuned frequency combined with optimized coil geometry. This approach significantly improves the metal detector's ability to differentiate actual metal contaminants from the product's own natural signals, resulting in fewer false rejects.
Why Choose METTLER TOLEDO?
METTLER TOLEDO offers purpose-built solutions tailored to meet the specific challenges of bulk product manufacturing. Our metal detectors use three High/Ultra-High Tuned Frequencies in combination with optimized coil geometry to enhance sensitivity and reliably detect metal contaminants in bulk products. To optimize performance, this technology enables users to switch between preset frequencies to improve metal detection while maintaining maximum uptime.
We partner with manufacturers worldwide to implement strong, validated inspection systems and processes that comply with Global Food Safety Initiative (GFSI) standards, including BRCGS, IFS, and retailer requirements.
SENSE™ Technology: Uses advanced software and sophisticated algorithms to analyze product signals and improve detection of ferrous, non-ferrous, and stainless steel metals
High-Tuned/Ultra-Tuned Frequency Performance: Employs three High-Tuned/Ultra-Tuned Frequencies and eDrive/eDrive PLUS technology to automatically switch between multiple preset frequencies for superior detection in products susceptible to bulk effect
Radio Frequency Interference (RFI) Shields (M55RB): Reduce external interference, significantly increasing sensitivity
Comprehensive Validation and Compliance Support: Systems feature automated test protocols, detailed reporting, and documentation tools to help meet BRCGS, SQF, and retailer standards
Durable Hardware for Tough Environments: Models like the M33RB and M55RB feature up to IP69K-rated housings for reliable operation in bulk processing areas with heavy washdown requirements
Global Expertise and Local Service: Our network of product inspection specialists offers application testing, installation support, and responsive for optimal system performance
Seamless Line Integration: We provide a range of aperture sizes and conveyor designs, including specialized solutions for smooth integration into existing bulk product lines
Core Technologies for Bulk Metal Detection
SENSE™ Software Platform
The SENSE™ software platform is the intelligent brain behind our metal detectors. It uses advanced digital signal processing and adaptive algorithms to continuously optimize detection settings. For bulk products that have natural variations, such as those with changing moisture or density, SENSE™ adapts to maintain consistent detection. The touchscreen interface is easy to use and helps make operator training more efficient.
Show more
eDrive / eDrive PLUS Technology
eDrive technology from METTLER TOLEDO improves sensitivity by creating a stronger detection signal. This allows the metal detection system to identify all types of metal, including hard-to-detect stainless steel, in products like seasoned flour, protein powders, and moist grains. It achieves high sensitivity while reducing false rejects and maintaining strict quality standards.
Bulk processing areas present tough conditions such as vibration, humidity, and frequent high-pressure washdowns. Bulk metal detectors from METTLER TOLEDO are built to handle these challenges. They have sturdy designs that reduce vibration interference, housings made of stainless steel or IP69K-rated polyurethane, and sealed connectors. For heavy-duty conveyor use with packaged bulk products weighing 50 to 110 pounds, the systems feature reinforced frames and belts. This durability supports continuous operation, lowers maintenance downtime, and shields internal components from harsh conditions.
What is Infinity? Infinity is an advanced electronic test system designed to verify metal detector performance without the need for physical test pieces or manual intervention. Electronic signals simulate metal contamination, including ferrous, non-ferrous and stainless steel 316, to confirm your metal detector continues to operate within specification. So, how does Infinity work? In standard performance monitoring routines, physical metal test samples are placed on or in products and passed through the metal detector. Infinity works differently. Instead of physical test pieces, it externally generates a precise electronic signal equivalent to your required test piece size when it is directly in the center of the aperture at different testing positions. By testing the center of the aperture performance, which is the weakest point of detection, it confirms worst case sensitivity of the metal detector. Testing can be triggered automatically or manually, delivering consistent, repeatable performance checks every time. So how will this benefit you? Compliance confidence. Infinity verifies and documents that your detector consistently operates within required sensitivity levels. Automation and efficiency. Reduce manual intervention. Improve consistency of testing and enhance operational reliability through automated testing. Up to three times faster testing. Complete verification up to three times greater. runs quicker than standard manual testing to improve ROI and reduce lost time, product waste, profit and people resources. Hygienic and safer process with no physical test pieces and no manual handling required, operator interaction is minimized and supports improved hygiene standards. Automatic data capture. Access automatically recorded test results that enhance traceability and strengthen audit readiness. Infinity is an auto test system that streamlines performance verification, increases productivity, improves compliance confidence and delivers reliable, repeatable testing for greater confidence that your metal detector performs exactly to specification. With Infinity, electronic test system moves to smarter metal detector testing. It's now available with our M50 - DRC's advanced line metal detectors.
INFINITY - Electronic Test System
INFINITY is an advanced Electronic Test System from METTLER TOLEDO designed to verify metal detector performance, without the need for physical test pieces or intervention. This auto test system streamlines performance verification, increases productivity and improves compliance confidence. The software process simulates metal contamination such as ferrous, non-ferrous, and stainless steel 316 through external electronic signals. Just like Performance Monitoring Routines (PMR), INFINITY provides peace of mind that the metal detector is operating within specification and supports compliance.
It is important to note that a full PMR process with physical test samples must still be carried out within the quarantine period as outlined in GFSI (Global Food Safety Initiatives) such as BRCGS or Retailer Codes of Practice. INFINITY is designed to complement PMR, not replace it.
Dry bulk products can cause a dry bulk effect and are often subject to vibration as they move along the production line. METTLER TOLEDO metal detection systems, equipped with Dynamic Stability Coils and SENSE™ software, offer high sensitivity to detect small metal fragments that may enter products from milling or processing equipment.
Nutritional Supplements and Seasoned Mixes
The combination of High/Ultra-Tuned Frequencies, eDrive technology, and SENSE™ software helps detect the smallest metal contaminants in fine-grained products such as protein powders, powdered nutritional supplements, and seasoned or fortified mixes.
Deep-Frozen Vegetables and Fruits
Our metal detectors use fast digital processing and High/Ultra-Tuned Frequency technology to maintain consistent and reliable detection sensitivity on high-speed production lines for deep-frozen vegetables and fruits.
Bagged and Boxed Goods
When inspecting packaged bulk products, such as large sacks of flour, there is the additional challenge of handling the packaging itself. Our conveyor systems are designed for large packages and include the most suitable reject devices for each application.
Bulk Metal Detection Downloads
Learn more about our bulk metal detection systems in our informative brochures and datasheets.
M55RB AdvancedLine Datasheet
The M55RB metal detector with optimized coil geometry improves sensitivity in bulk products, such as large sacks, bags of powder, and cartons.
Download the datasheet to learn more.
M50 R-Series AdvancedLine Brochure
The M50 R-Series metal detectors are our most digitally advanced range for outstanding sensitivity and performance in wet, challenging, dry and bulk products.
Download the brochure to learn more.
The M55RB is part of the M50R series advanced line and is the latest metal detection solution from Mettler Toledo. Engineered on our most digitally advanced platform, it delivers exceptional sensitivity and reliable performance for bulk or large product inspection across many industries and applications, such as large sacks of flour, bags of powder and cartons. With an optimised coil geometry, ultra high tune frequency up to 900 kHz and eDrive plus technology, you can detect smaller metal contaminants and deliver safer products with confidence. Radio frequency interference shields filter out and reduce external interference in large aperture applications, significantly enhancing sensitivity. You can detect the smallest metal contaminants, delivering safer products with confidence. A hygienic design, up to IP69K rating, with curved corners and sloping surfaces allow quick and easy cleaning to support regulatory standards including BRCGS, IFS and HACCP. Infinity. Electronic test system significantly advances routine testing, supporting performance monitoring routines, reducing test time and line stoppages to keep good products moving and maximise uptime. Embedded Wi-Fi provides secure, simple access to system data. No complexity, just instant information on your mobile device. And with the 10.1-inch HMI touchscreen, navigation is easy – even with gloves or in wet environments. You protect more than products. RFID access control gives the right people the right level of control, while the integrated service QR code provides fast access to expert support anytime. Products Complete inspection management and connectivity software solution from Mettler Toledo Automates essential processes including monitoring, reporting and data collection of all product inspection activities in real time M50 R-Series Advanced Line Your partner from the production line to the world
AdvancedLine metal detector provides exceptional performance to deliver safer bulk or large products. Your partner to protect your brand and support your compliance requirements.
PlusLine metal detector with optimized coil geometry and high, tuned frequency technology. An affordable compliance solution for inspecting large or bulk products on a conveyor.
What is bulk effect, and why does it make metal detection harder?
Bulk effect happens when inspecting large volumes of products, such as sacks, cases, or crates, which can reduce the sensitivity of the metal detector. Essentially, the bulk material itself creates a signal that interferes with the detector's ability to distinguish metal contaminants. This lowers the detector’s sensitivity, making it harder to spot smaller metal pieces in the bulk product. To address this issue, manufacturers can select a metal detection system designed to reduce bulk effect and increase detection sensitivity in bulk foods.
METTLER TOLEDO offers metal detectors with three High/Ultra-High Tuned Frequencies. This technology improves sensitivity for bulk product inspection by allowing the system to switch between preset frequencies. The result is better detection of metal contaminants in bulk products.
How does multi-frequency technology improve metal detection in bulk foods?
Multi-frequency technology sends and analyzes several frequencies at the same time. This helps the metal detection system build a clear profile of the product’s natural signals and remove them from the measurement. As a result, the detector produces a stronger signal for metal contamination and can operate with greater sensitivity, even in bulk products.
What role does metal detection software like SENSE™ play in detecting contaminants in bulk products?
SENSE™ software acts as an intelligent filter and optimization tool. It uses advanced algorithms to adjust the metal detector’s settings in real time, responding to natural variations in the product such as moisture levels. This helps the system make quick decisions to detect small metal particles that might otherwise be missed, reducing false rejects and product waste.
Where is the best place to install a metal detector on a bulk product line?
The best location depends on where metal contamination is most likely to occur. Common points include raw material intake and the stages after major processing steps, such as milling or mixing, but before final packaging. For bulk powders, install the detector where product flow is steady and free of air pockets. On conveyor lines, place the detector on a stable section that minimizes vibration.
METTLER TOLEDO technicians can conduct a site survey and recommend the best location and installation method for optimal detection and reliability.
Elham holds a Doctorate in Pharmacy (PharmD) and a Master of Science (MSc) in Marketing, blending scientific knowledge with market insight. Since starting her career in 2017 in the pharmaceutical industry, Elham has worked mainly in the pharmaceutical, chemical, and industrial technology sectors. She leads projects that connect purpose, people, and performance. Her focus is on linking technical excellence with clear and compelling communication to improve commercial results and build long-term brand value. Currently, Elham is the Global Marketing Manager for the Metal Detection Strategic Business Unit (SBU) at METTLER TOLEDO. She works closely with international and cross-functional teams to strengthen brand positioning, lead global initiatives, and support sustainable business growth in diverse markets.
Request Quote or InfoGet a QuoteInstant QuoteSolution InformationRequest a Demo
I want to…
Need assistance? Our team is here to help you achieve your goals! Speak with our experts.